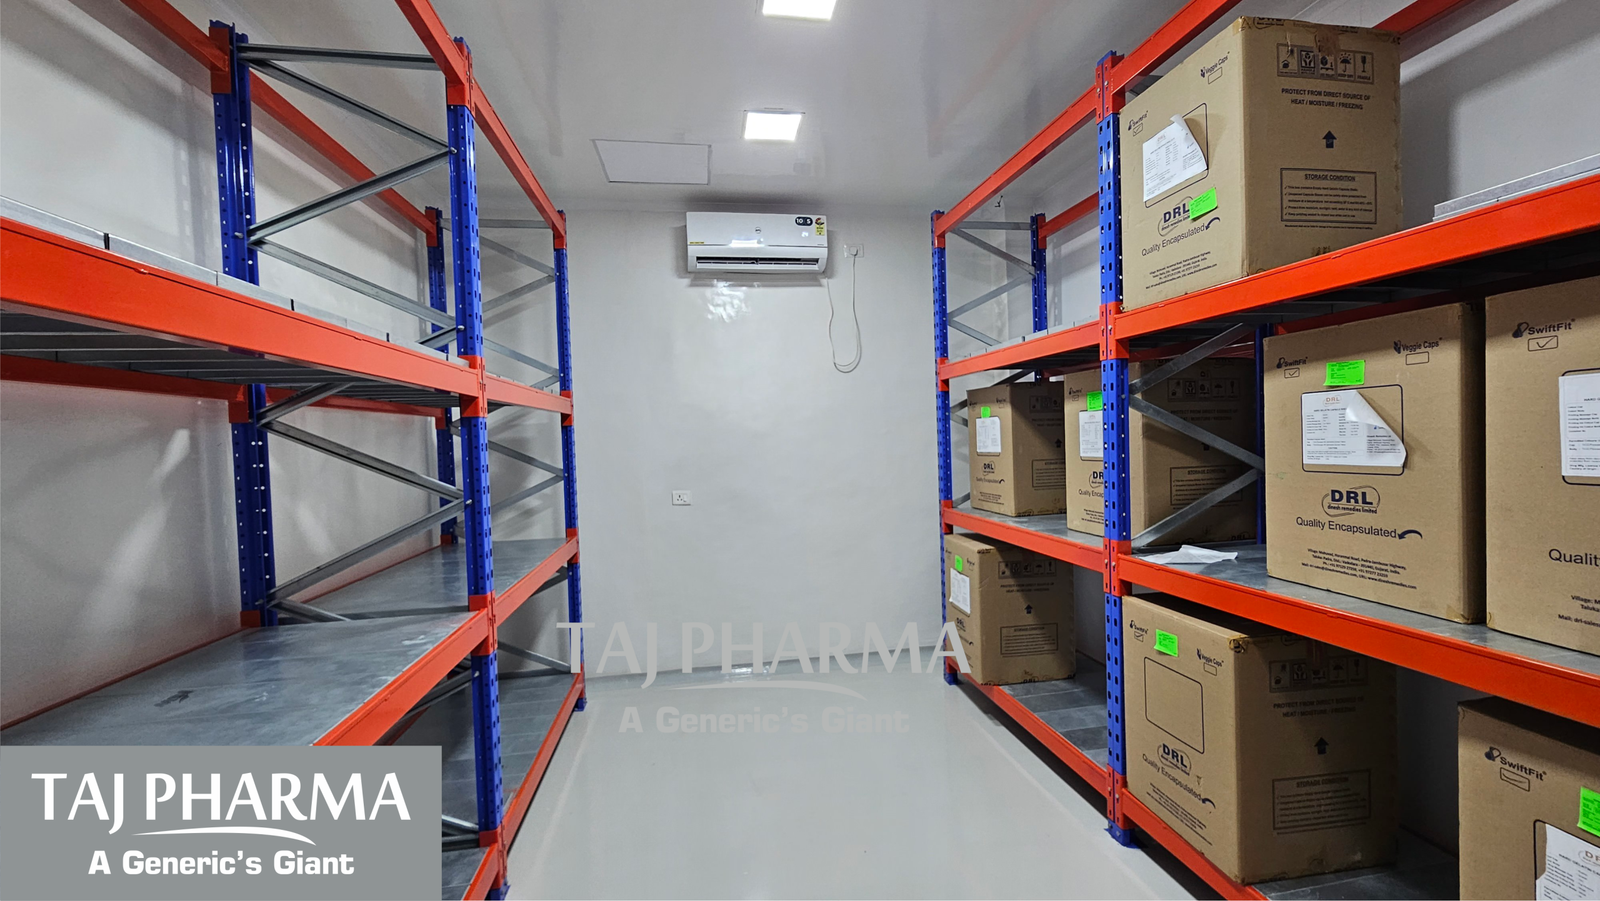
Description: The Sarigam plant integrates cutting-edge technology and automation systems that enhance both production efficiency and data integrity. With automated blending, granulation, and coating systems, coupled with high-speed tablet compression and encapsulation machinery, the facility minimizes manual intervention while maximizing process consistency. The HVAC-controlled cleanroom environments maintain optimal temperature, humidity, and pressure differentials to ensure sterile and contamination-free manufacturing. Every stage of production is digitally monitored and validated through 21 CFR Part 11 compliant systems, ensuring transparency and traceability from raw material to finished product. Analytical and Microbiology Laboratories: Guaranteeing Product Integrity Quality assurance is at the heart of Taj Pharma’s operational philosophy. The Sarigam facility houses state-of-the-art analytical and microbiology laboratories, fully equipped to perform: Raw material and finished product analysis In-process quality control tests Stability studies under ICH guidelines Microbial limit and sterility testing Validation and environmental monitoring programs These labs are staffed with qualified scientists and microbiologists who ensure every product batch meets the highest standards of potency, purity, stability, and safety before release. Each analytical process is aligned with USP, BP, IP, and EP pharmacopeial standards. Commitment to Research and Development (R&D) Taj Pharma’s R&D division operates as a catalyst for innovation in formulation development and technology transfer. By focusing on bioequivalent generic formulations and novel drug delivery systems (NDDS), the company continuously enhances its product portfolio. Research efforts are directed toward cost-effective, stable, and patient-centric formulations, empowering the company to meet evolving global healthcare needs. From oral solid dosage innovations to topical and nutraceutical formulations, Taj Pharma’s R&D unit ensures the company remains a front-runner in pharmaceutical advancement.
Dimensions: 2560 x 1442
File Type: png
File Size: 4 MB