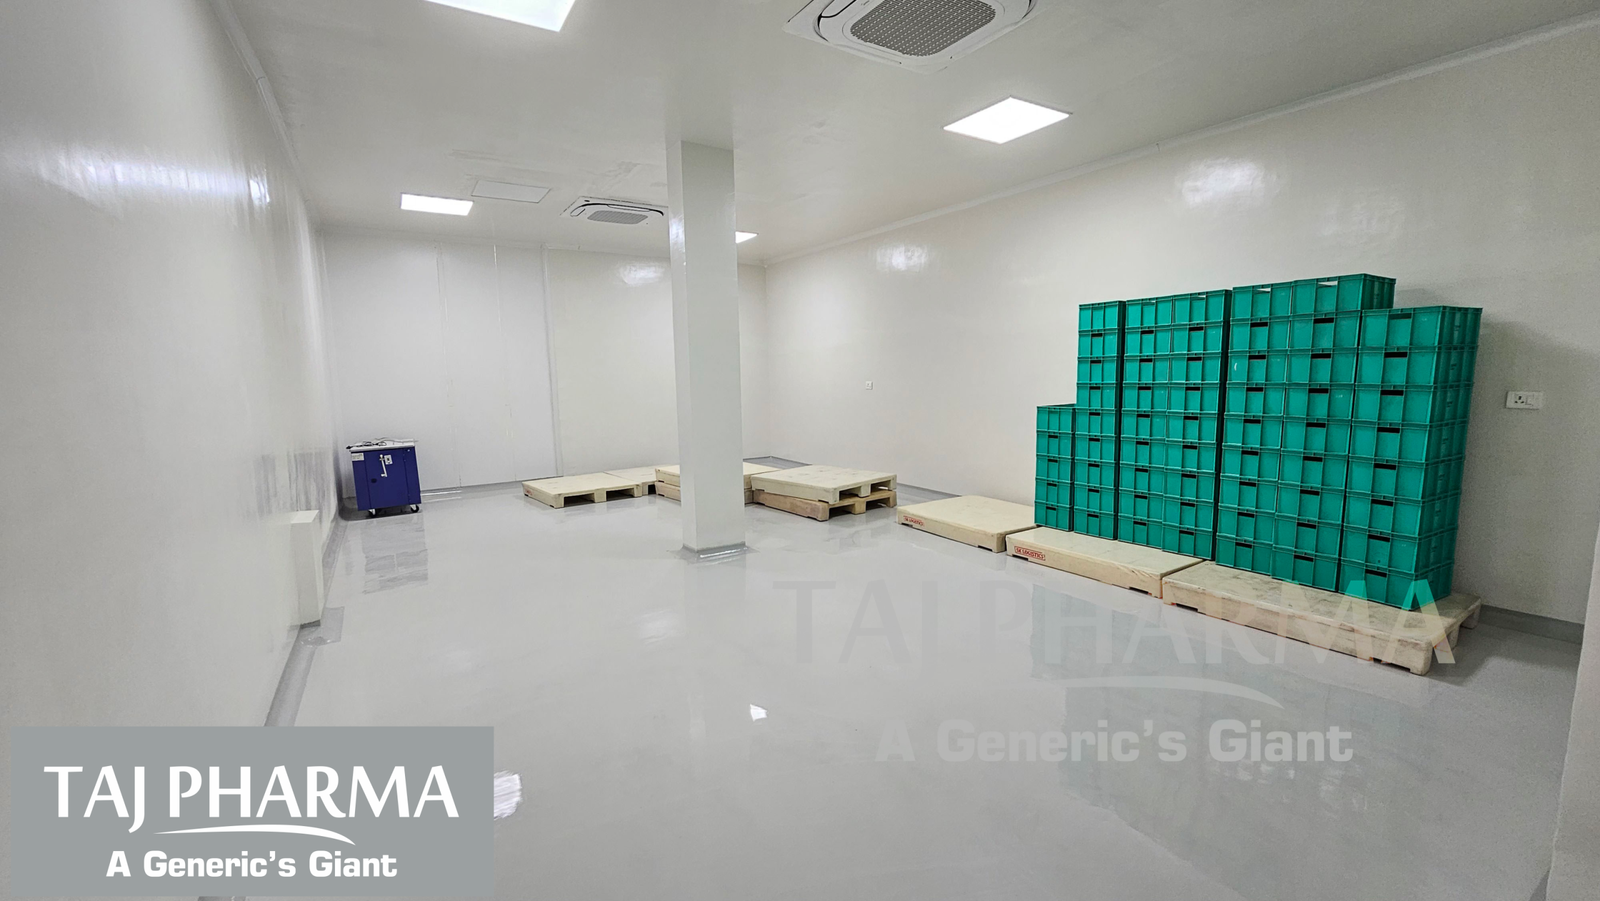
Description: Taj Pharma India Ltd. follows strict quarantine storage procedures to ensure that all raw materials, packaging materials, intermediates, and finished pharmaceutical products meet the highest standards of quality, safety, and compliance. The quarantine storage area at Taj Pharma’s Sarigam manufacturing facility is designed with controlled temperature, humidity, and segregation systems to prevent any cross-contamination or mix-ups during storage. All incoming materials are carefully inspected and labeled as “Under Quarantine” until they pass the required Quality Control (QC) testing and are formally released by the Quality Assurance (QA) department. This process ensures that only approved and tested materials move forward for production or dispatch. The storage areas are monitored using advanced barcode and computerized inventory systems, ensuring complete traceability and accountability throughout the supply chain. Taj Pharma’s quarantine storage management strictly adheres to WHO-GMP and ISO 9001:2018 guidelines, maintaining the integrity and safety of pharmaceutical products. Each section is regularly audited and validated to ensure compliance with cGMP standards. By implementing these robust quarantine measures, Taj Pharma India Ltd. guarantees that every product manufactured and distributed is pure, compliant, and of premium quality, reinforcing its global reputation for pharmaceutical excellence and reliability.
Dimensions: 2560 x 1442
File Type: png
File Size: 3 MB